
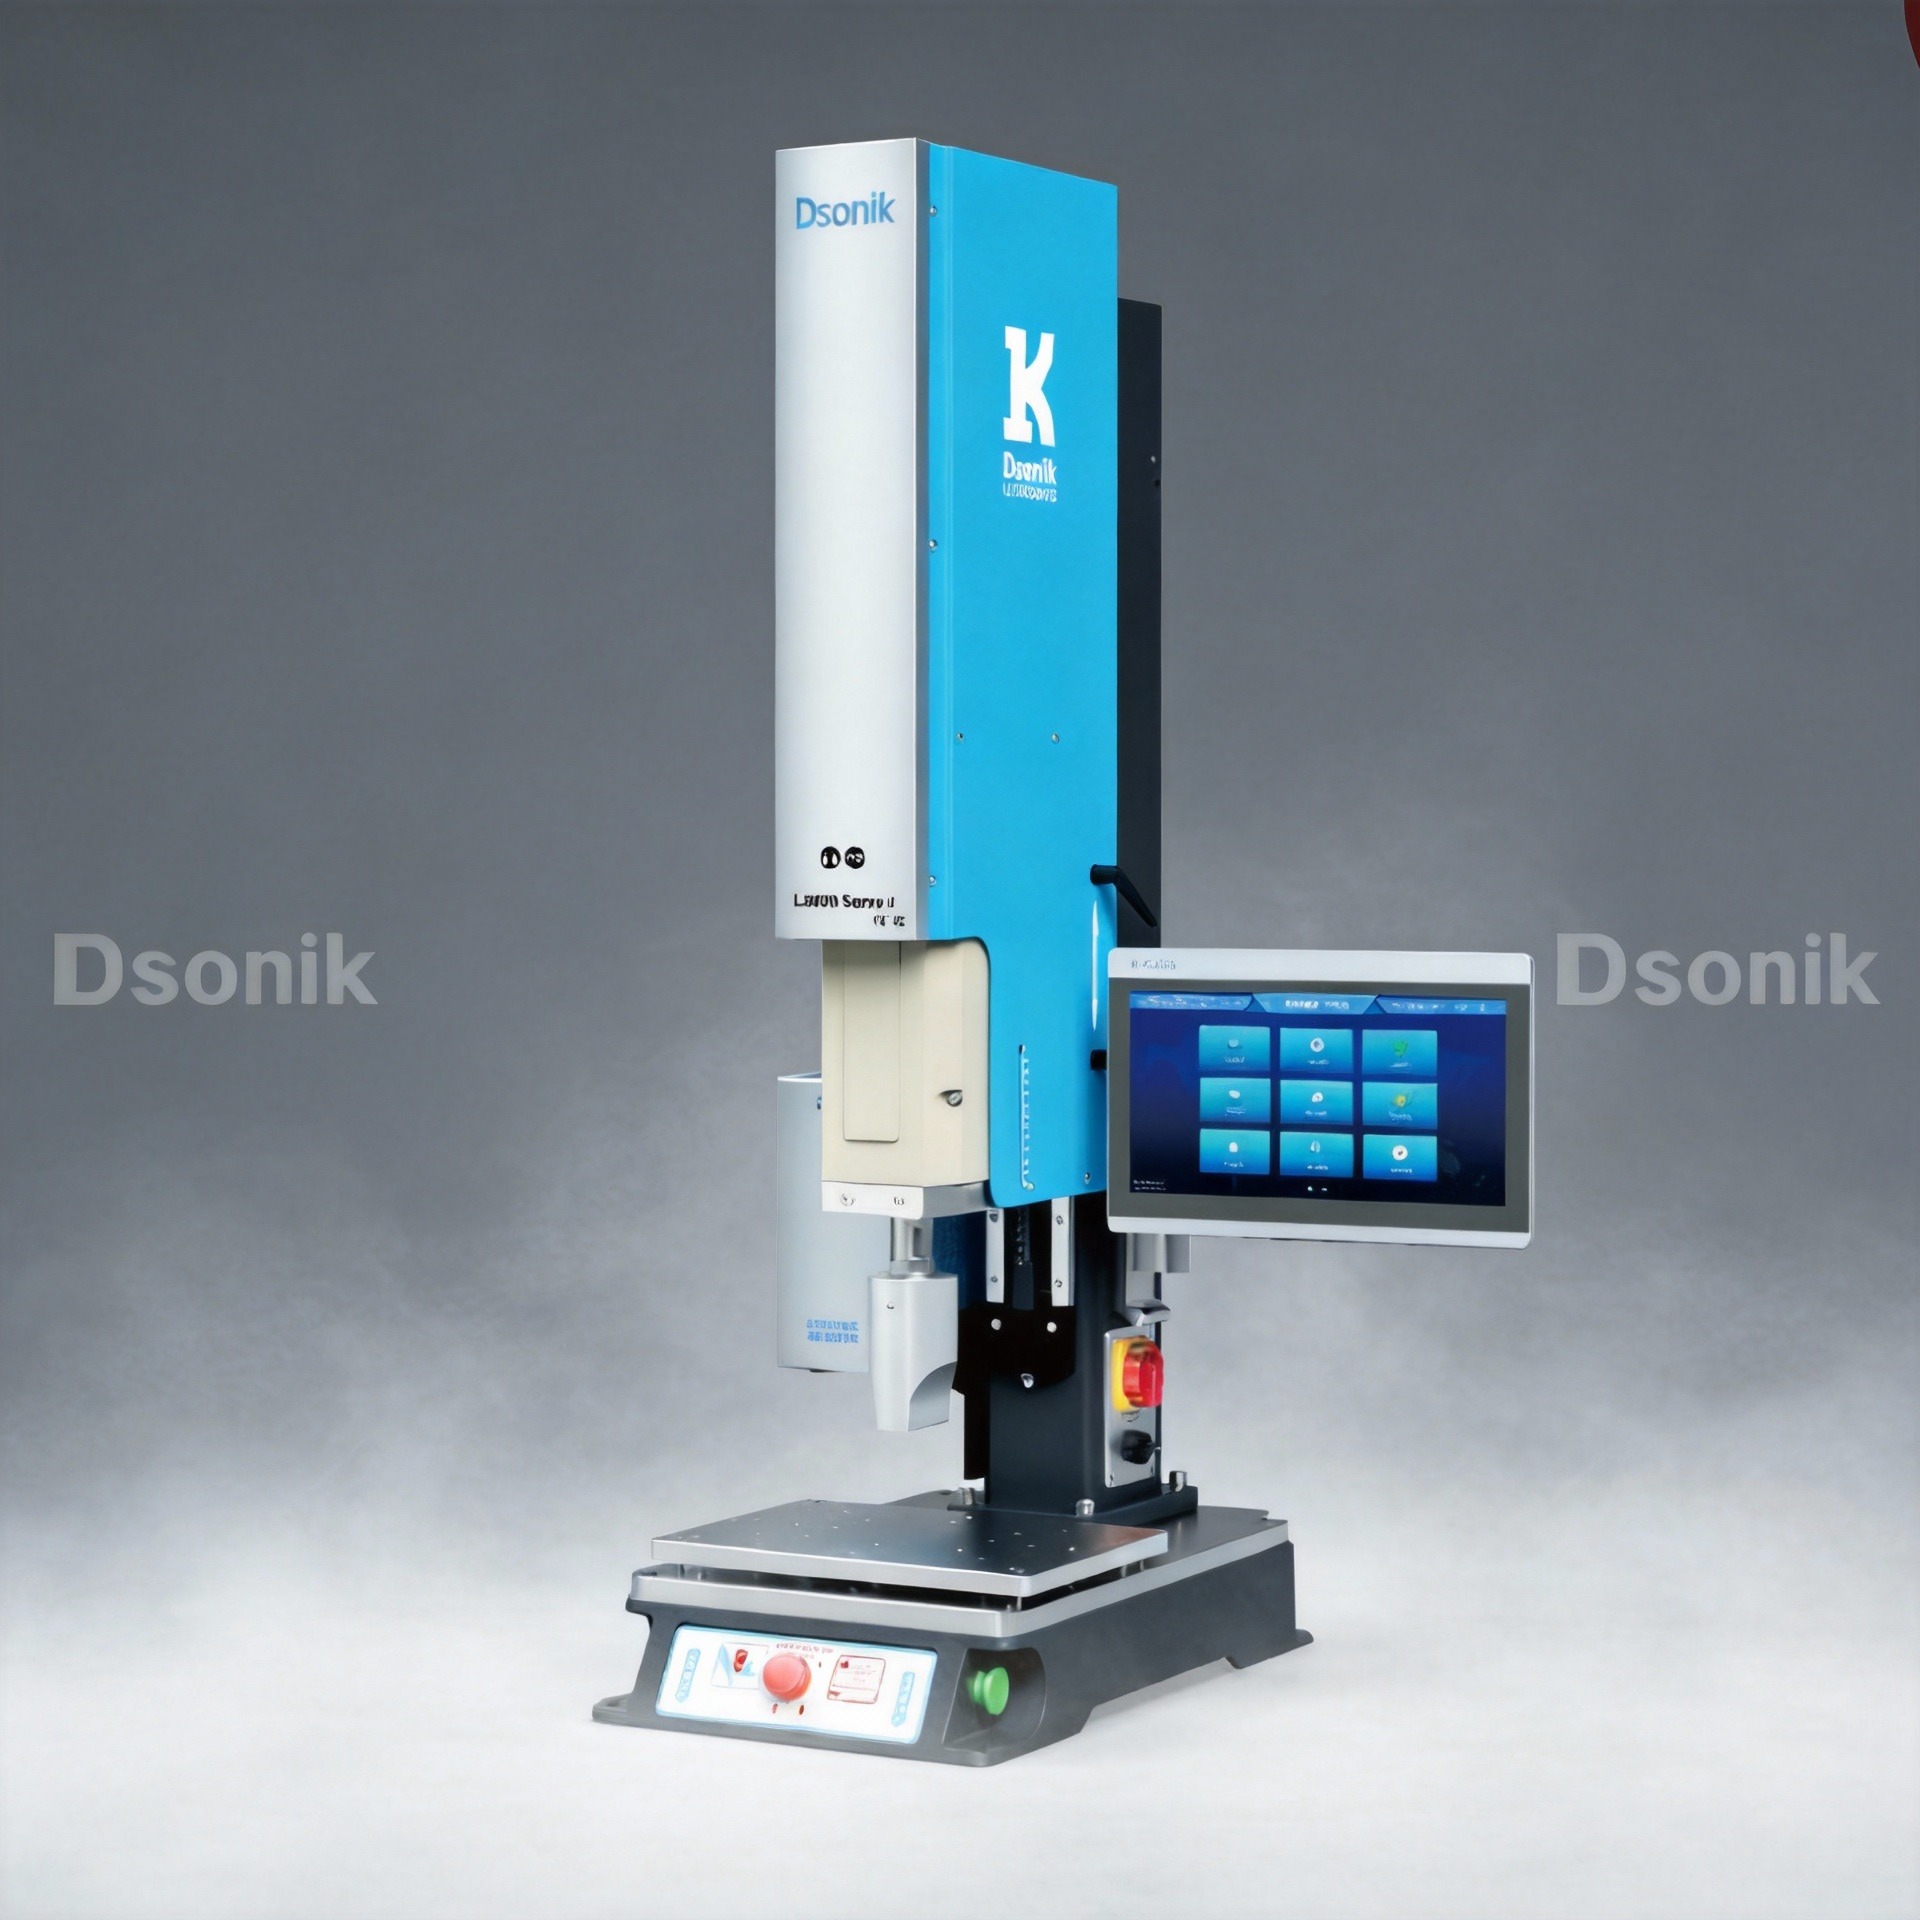
How to Set the Ultrasonic Horn and Fixture in a Plastic Welding Machine
Correct horn and fixture setup is essential for reliable ultrasonic plastic welding. Even with suitable process parameters, poor alignment can cause weak joints, leakage, surface marks, cracks, uneven welds, and premature horn failure.
Recommended Horn and Fixture Setup Procedure
1. Install the horn correctly. Thoroughly clean the mating surfaces of the booster and horn. They must be flat, dry, and free of oil, plastic particles, scratches, and burrs. Tighten the horn to the manufacturer’s specified torque, and never apply tightening force through the converter or transducer body.
2. Initially leave the fixture loose. Position the lower fixture on the machine table without fully tightening its mounting bolts, then place a known-good production part in it.
3. Lower the horn slowly. Keep ultrasonics OFF. In manual or jog mode, lower the horn until it just touches the upper component. Do not allow the horn to strike the part.
4. Self-align the fixture. With the horn lightly touching the component, allow the loose fixture to center itself naturally beneath the horn. The part should remain free of lateral force and distortion. Carefully tighten the fixture bolts without shifting its position.
5. Verify full horn contact. The horn should contact the component uniformly across its entire face, not only at one side or at isolated high points. For larger parts, use thin contact or pressure-indicating paper to identify uneven loading.
6. Check parallelism. Align the horn face, plastic components, weld joint, and fixture. If one side contacts first, correct the fixture position, level, part seating, or tooling geometry rather than increasing weld pressure.
7. Confirm fixture support. Support the lower component firmly beneath and around the weld joint to prevent flexing during vibration. However, do not clamp it so tightly that necessary vibration or melt flow is restricted.
8. Check horn clearance. Throughout the full weld stroke, the horn must not contact the fixture, metal inserts, ribs, or any unintended area. Account for the expected weld collapse, not just the starting position.
9. Set the mechanical stop or stroke. If the machine uses a mechanical stop, allow enough travel for the required weld collapse while preventing excessive part compression.
10. Run low-energy trial welds. Begin with conservative settings and inspect for uniform collapse, consistent flash, surface marking, cracks, and incomplete fusion. Do not use maximum amplitude or an excessive weld time to compensate for tooling problems.
A Correct Setup Should Follow This Arrangement
Horn / Sonotrode
↓ Uniform vertical force
Upper plastic part
══════════ ← Weld joint / energy director
Lower plastic part
██████████ ← Properly supported fixture
Machine table
Horn and fixture alignment is especially important for leak-tight PC welding. Even a slight horn tilt or uneven fixture support can cause the energy director to collapse more on one side, leaving a microscopic unwelded path—and a potential leak—on the other.
A useful rule for DSONIK applications is:
Do not use ultrasonic parameters to correct a mechanical tooling problem. First establish uniform horn contact, adequate fixture support, parallelism, and proper part alignment. Then optimize amplitude, force, energy or collapse, and hold time.